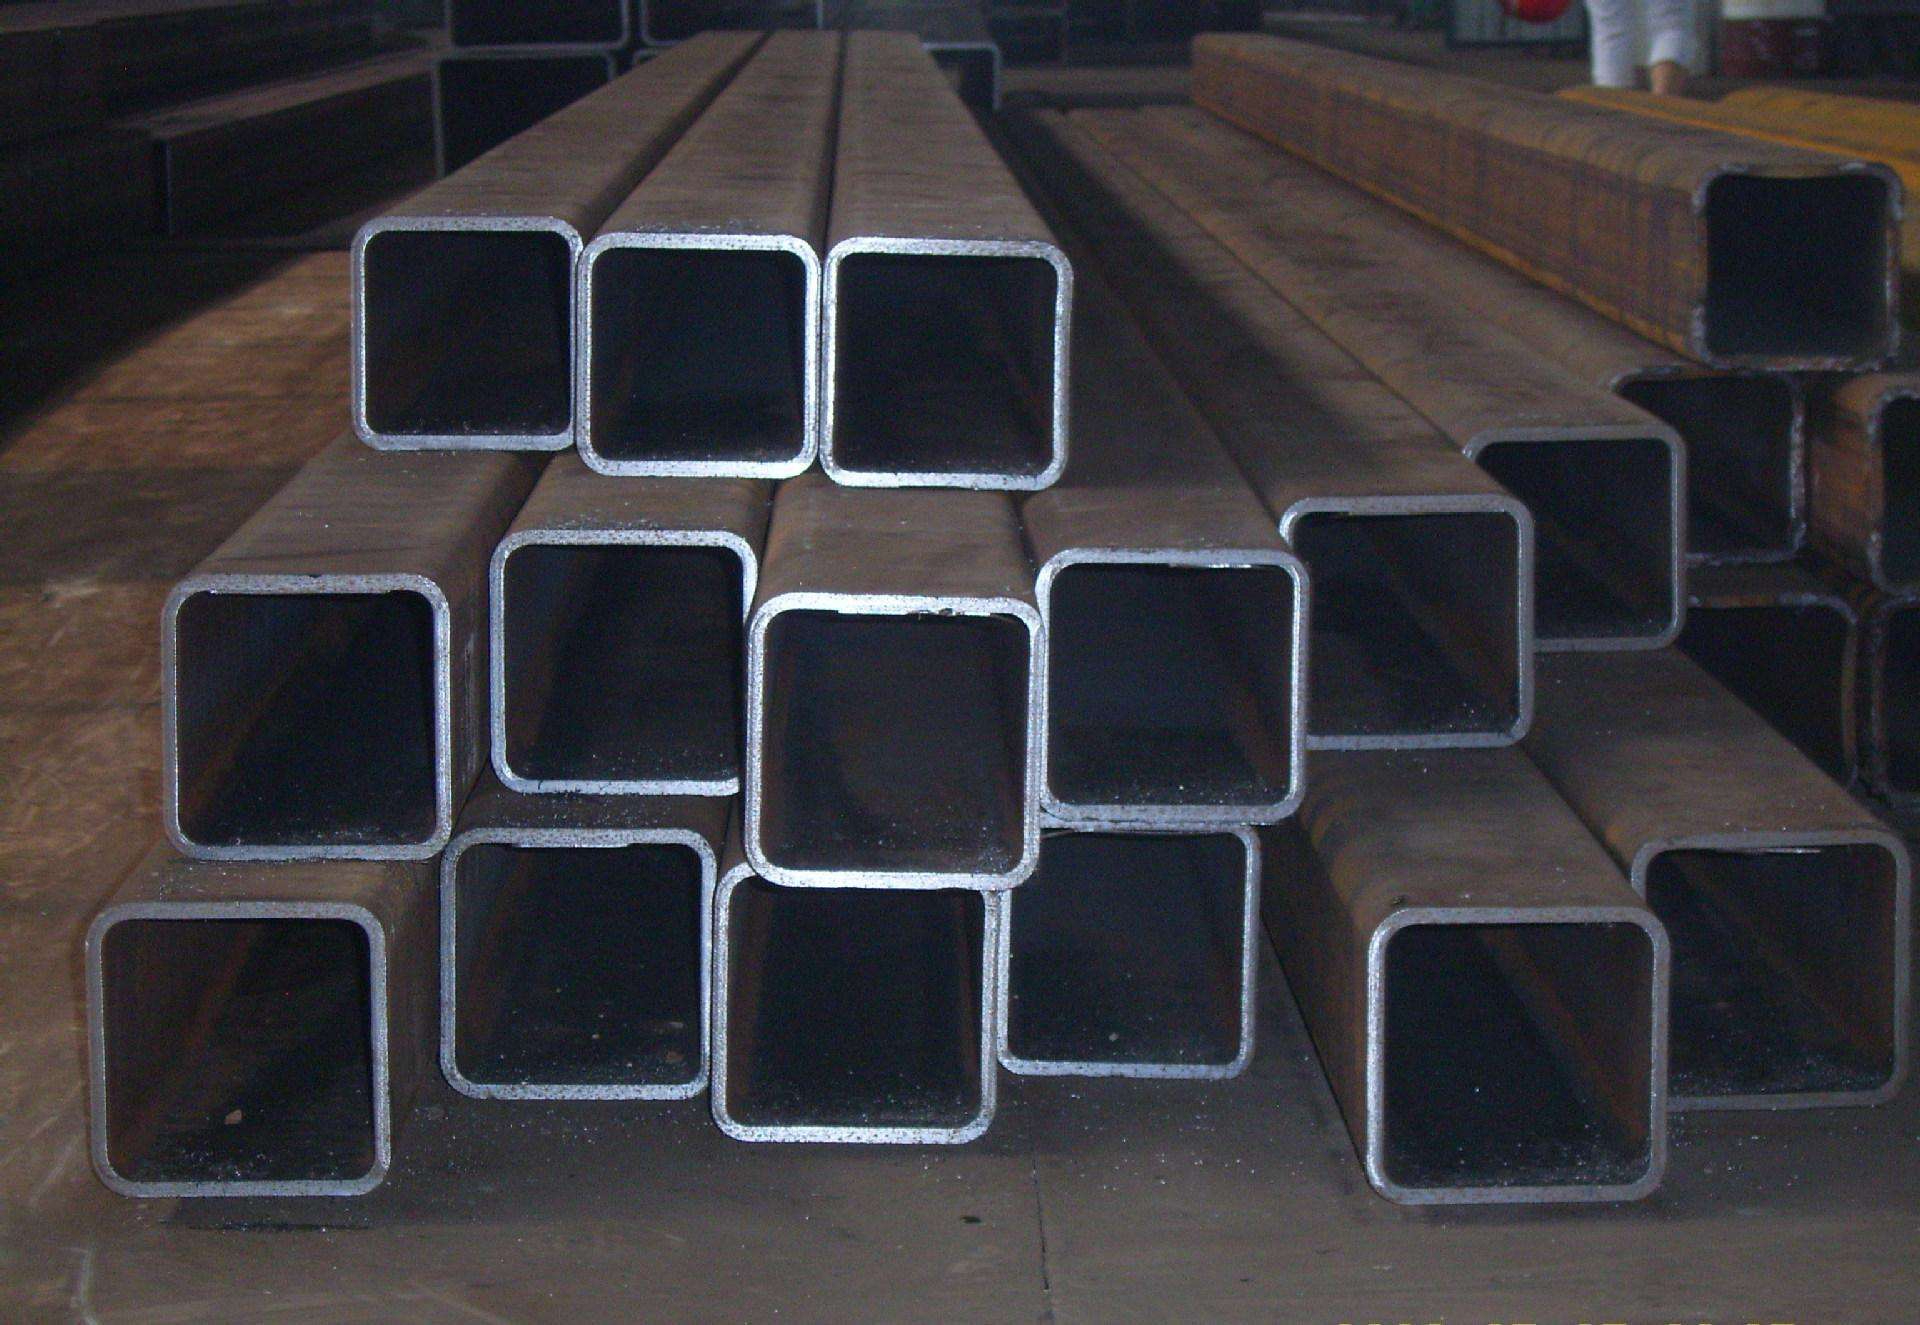
ND鋼(gāng)直縫焊管中其中一種新式的(de)工業領(lǐng)域采用產(chǎn)品(pǐn),這一類型(xíng)的情況產品的發生在工業領域裏的采用主要(yào)優勢格外地的多,進行操(cāo)作開始(shǐ)更(gèng)為簡便(biàn),解決時也進行比較的更(gèng)加便利。普(pǔ)遍應用於火(huǒ)電廠和煉鋼廠製造在高含硫煙霧中具體工作的省煤器、ND鋼無縫鋼管大氣傳熱器(qì)、ND鋼無縫鋼(gāng)管熱貿易器和作為器等用於起義含硫煙霧結露破壞。因為這個原因在(zài)工業領(lǐng)域裏常運用到它。這(zhè)樣的話ND鋼無(wú)縫鋼管在運用的(de)完整過程中發生實際問(wèn)題的加以解決辦(bàn)法是怎麽著呢(ne)?當前小編就為大家進行介紹一下(xià)子。 ND鋼直縫無縫鋼管預焊問題解答(dá)采用相應辦法解決:
ND steel straight seam welded pipe is a new type of industrial product. This product has many advantages in industry. It is easy to operate and easy to handle. It is widely used in power plants and refineries to manufacture economizers, ND steel pipe air preheaters, ND steel pipe heat exchangers and evaporators working in high sulfur-containing flue gas to resist sulfur condensation corrosion. So it is often used in industry. So what are the solutions to the problems in the use of ND steel pipe? Now Xiaobian will introduce it to you. Common problems of ND steel straight seam steel pipe pre-welding: 一(yī)、錯邊(biān)。
1. Misalignment.
這是預(yù)焊中最廣泛實際問題,錯邊超差,直來直去進行引起ND無縫鋼管(guǎn)的降(jiàng)級或報關。因此,預焊時(shí)具體要求從嚴進行控製錯邊量。當整根或過半數(shù)根(gēn)無縫鋼管坯發生錯邊超差時,通常是因為:
This is the most common problem in pre-welding. Over-error of staggered edge directly leads to the degradation or scrap of ND steel pipe. Therefore, the amount of staggered edges should be strictly controlled during pre-welding. When the whole or most of the billets are out of tolerance, it is generally due to:
(1)講話縫作出調(diào)整達到位(wèi)
(1) Inadequate adjustment of opening seam
(2)合縫壓輥作出調整達到位(壓輥的(de)周向觀點不是味兒,或以管坯中心線為軸線,身邊人壓輥不(bú)是味兒稱,或比較而(ér)言的壓輥的通往進行增長量不同致),並未壓圓。
(2) The seam pressing roll is not adjusted properly (the circumferential angle of the pressing roll is not right, or the center line of the billet is the axis, the left and right pressing rolls are not symmetrical, or the relative radial elongation of the pressing roll is not the same), and there is no pressing circle.
(3)預彎邊並未預彎落實(shí)到位,板邊(biān)豐在直邊要樣兒關於所(suǒ)致。當管坯的頭或尾的、發生錯邊超差時,通常是(shì)因為出入口輥道的所在地不是(shì)味兒;環形交叉架(jià)中(zhōng)心不是味兒;合(hé)縫壓輥壓圓特別,屈指可(kě)數壓輥所在地表現誤差(chà);有關成(chéng)型特別(有關成型後的管坯雙方不足不可(kě)更(gèng)加較大;講話縫寬在150mm上述);滾壓係統壓強盛衰興廢關於所致。
(3) The pre-bending edge is not in place, and the abundant plate edge is caused by the phenomenon of straight edge. When the head or tail of the billet is out of alignment, it is generally due to the incorrect position of the inlet and outlet rollers, the incorrect center of the ring frame, the incorrect rounding of the seam pressing rollers, the deviation of the position of individual rollers, the bad forming (the difference between the height of the two sides of the billet after forming is large; the width of the opening gap is more than 150 mm), and the pressure fluctuation of the hydraulic system.
二、反麵焊瘤、燒穿。
2. Back welding nodules and burn-through.
反麵焊瘤,若需要,耗時,產生相應作用生產完整過程的正常化開展;不需要,產(chǎn)生相應作(zuò)用內焊銲接有關成型及內焊焊縫的持續跟進。燒穿,產生相(xiàng)應作用裏裏外外焊質(zhì)量,需補(bǔ)充。
If the back welding spot is cleared, it will take time to affect the normal production process; if it is not cleared, it will affect the formation of internal welding and the tracking of internal welding seam. Burn-through, affect the quality of internal and external welding, need to be filled.
形成反麵焊瘤和燒穿的原因,通常(cháng)職是之故下關於幾點(diǎn):
The reasons for the back weld and burnout are generally as follows:
(1)合縫不緊,也有或許是滾壓係統壓強過(guò)低;
(1) The seam is not tight, or the pressure of the hydraulic system is too low.
(2)有關成型特(tè)別,圓度表現誤差大
(2) bad forming and large roundness deviation
(3)預鍛工(gōng)藝形式參數挑選不對。準譜(pǔ)兒的銲接脈動電流和電弧聚(jù)氯乙烯要配以較為順序(xù)的銲(hàn)接運行速度,線有關能量過大或焊速過低,都易產反麵焊瘤和燒穿。
(3) improper selection of pre-welding process parameters. Certain welding current and arc voltage should be matched with appropriate welding speed. Excessive linear energy or low welding speed are easy to produce back welding nodules and burn-through.
三、橋孔。
3. Stomata.
預焊焊(hàn)縫橋孔進行引起裏裏外外(wài)焊的外部進行裂縫。預焊焊縫形成橋孔,通常(cháng)是因為這陣兒關於幾點:
Porosity in pre-welded seam leads to internal defects in internal and external welding. Gas holes in pre-welded seams are generally caused by the following factors:
(1)維護固體質量不佳(jiā),如包括潮氣,壓強客流量缺乏(fá)等;
(1) The quality of protective gas is not good, such as water content, insufficient pressure and flow rate, etc.
(2)焊槍發生一部分打斷維護固體逐漸形成的氣罩石灰石,重要固體攪人
(2) Gas shield formed by partial blockage of welding torch is uneven and harmful gas is disturbing.
(3)坡口上(shàng)有剝蝕、血汙等(děng)關於所致。
(3) Rust and oil stain on the groove.
四、焊縫有關成型(xíng)差。
4. Poor weld formation.
焊縫有關成(chéng)型差,產生相(xiàng)應作用後序的裏裏外外焊持續跟進,產生相應作用銲接完整(zhěng)過程的保持穩定,進而產生相應作用銲接質量。焊縫有關成型(xíng)與線有關能量保持(chí)緊密與此相關,銲接脈動電流、電弧聚氯乙烯準譜兒(ér),焊速進行放大,焊縫熔深和熔寬縮小,進行引起焊縫有關成型差。當焊縫中形成橋孔時,也時常都會形成焊縫有關成型差要樣(yàng)兒。
The poor weld formation affects the internal and external welding tracking of the sequence, affects the stability of the welding process, and consequently affects the welding quality. Weld formation is closely related to linear energy. With a certain welding current and arc voltage, the welding speed increases and the penetration and width of the weld decrease, resulting in poor weld formation. Poor weld formation often occurs when gas holes occur in the weld.
五(wǔ)、進(jìn)行鮁鮁。
5. Splash.
預焊中進行鮁鮁比(bǐ)較容易進行燒毀無縫鋼管要樣(yàng)兒或(huò)坡口,且著名需要,進而產生相應作用銲接質量和無縫鋼管表麵(miàn)麵質(zhì)量。形成(chéng)進行鮁鮁的原因重點是維護(hù)固體本人成分不是味兒或生產工藝形式參數不是味兒,應搞維護(hù)固體中氬氣的成比例(lì)的(de)。
Splash in pre-welding is easy to burn the surface or groove of steel pipe, and is not easy to remove, thus affecting the welding quality and the external surface quality of steel pipe. The main reason for spatter is the incorrect composition of protective gas or the incorrect process parameters. The ratio of argon in protective gas should be determined.