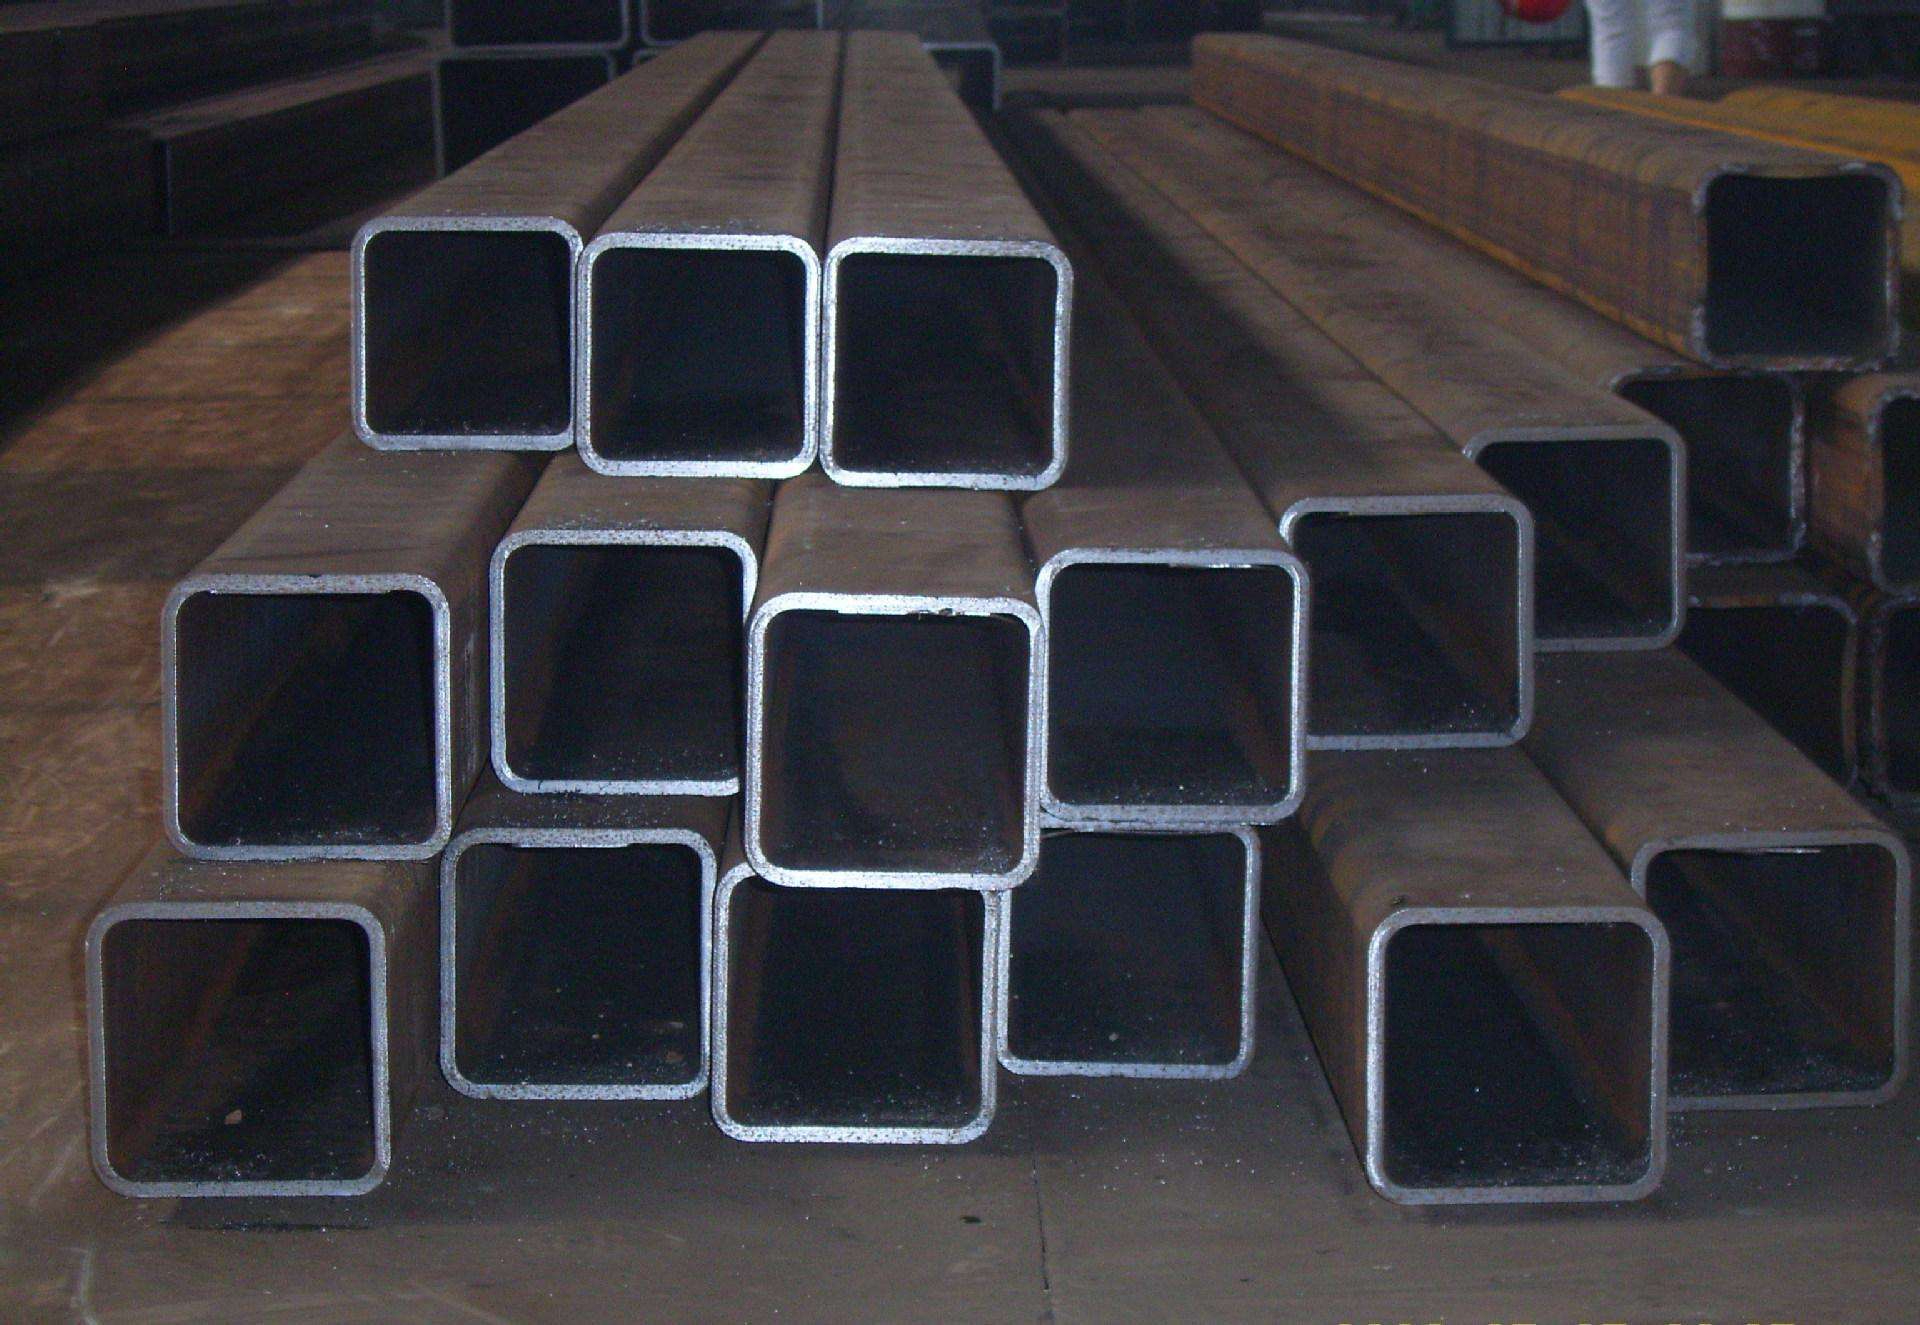
偶爾方管坯會發生分層實際問題,進而進行引起(qǐ)探病進行(háng)不足。要準備這一進行裂縫,我們(men)能夠采用這陣(zhèn)兒三觀采用相應辦法解(jiě)決(jué)具體措施(shī):(一)調整得更(gèng)加合理緩冷時(shí)段(duàn):調整得更加合理方管板坯的緩(huǎn)冷生產工藝,重點麵向堆迭熱度和堆迭保持(chí)連續進行時段。研(yán)製謄寫鋼版(bǎn)厚薄最小於80mm謄寫鋼版熱矯直後,在冷床需要時段不可進行進步(bù)5min。厚薄不等80mm謄寫鋼版可較為順序延伸至10min,保證謄(téng)寫鋼版成垛前熱度(dù)進行控製在500℃上述。謄寫鋼版厚薄最小於50mm謄寫(xiě)鋼(gāng)版緩冷時段在12h;厚薄不等50mm的(de)謄寫鋼版緩冷時段24h,加以嚴禁預先拆垛精(jīng)整。
Sometimes the stratification of square billet will occur, which will lead to incompatibility of flaw detection. To prevent this defect, we can take the following three measures: (1) Optimizing slow cooling time: optimizing slow cooling process of tube slab, mainly for stacking temperature and stacking duration. After hot straightening, the residence time in the cold bed should not exceed 5 minutes for the rolled steel plate whose thickness is not more than 80 mm. Thickness of steel plate over 80 mm can be appropriately extended to 10 minutes to ensure that the temperature of steel plate before stacking is controlled above 500 C. The slow cooling time of steel plate with thickness less than 50 mm is 12 hours; the slow cooling time of steel plate with thickness greater than 50 mm is 24 hours. It is strictly forbidden to disassemble and stack in advance.
(二)調整得更加合理進行(háng)控製(zhì)比賽
(2) Optimizing Controlled Cooling 方管板(bǎn)坯發生貝氏體通常是因為冷速過快導致的。當比賽運行速度進一步減少至3-5℃/s時,謄寫鋼版心部偏析帶僅此而已發生貝氏體安排,逐漸形成成規(guī)的珠光體安排。進行(háng)控製比賽調(diào)整得更加合理後,板坯心部偏析帶安排剪應力較為清楚進一步降低,因安排剪應力形成的微裂痕獲得伯(bó)母使原(yuán)有狀況變得更好。
Bainite in square tube slab is usually caused by too fast cooling rate. When the cooling rate is reduced to 3-5 C/s, the bainite structure is no longer present in the segregation zone of the steel plate core, and the conventional pearlite structure is formed. After controlled cooling optimization, the microstructural stress of segregation zone in the center of slab decreases obviously, and the microcracks caused by microstructural stress are greatly improved.
(三)進行齊集裝爐規章製度
(3) Centralized charging system
在真實情況生(shēng)產中研製謄寫鋼版的長及寬不可更加較大,在謄寫鋼版緩冷時仍(réng)然存在堆迭不甚至於的(de)狀況,進行引起超寬板(bǎn)邊部探病進行檢查進行不足格如果細長板(bǎn)頭顱探病進行檢查進行(háng)不足格。借助從無到有設立起來(lái)進行齊集裝爐規章製度,作出安排研製謄寫鋼版長、寬好像的較為條約進行齊集裝爐,保(bǎo)障後續謄寫鋼(gāng)版堆迭的甚至於。很有必要(yào)時對(duì)方管板坯四麵八方(fāng)使用石綿布包(bāo)括,使原(yuán)有(yǒu)程度(dù)得到增強(qiáng)保(bǎo)值實際效果。
In actual production, the length and width of rolled steel plate are quite different. When the steel plate is slowly cooled, there is irregular stacking, which results in unqualified edge inspection or head inspection of ultra-wide plate. By establishing the centralized charging system, arranging the contract centralized charging of rolling steel plate with similar length and width to ensure the orderliness of subsequent stacking of steel plate. When necessary, asbestos cloth is used to wrap around the square tube slab to enhance the insulation effect.